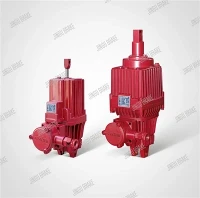
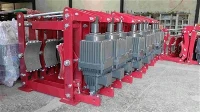
The two SBD-250-A-1320X30 I RL safety disc brakes required by the customer, along with the supporting YZ-15-20 hydraulic power unit, have been loaded onto the truck and dispatched.

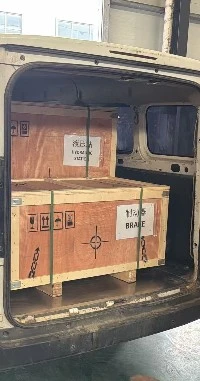
Prior to shipment, each product undergoes multiple quality inspection processes, covering core procedures such as braking performance testing, sealing inspection, and appearance protection checks. Every brake is securely packed in a custom wooden case, with the equipment name and shipping marks (including warnings for fragile, moisture-proof, etc.) clearly labeled on the outside of the crate, ensuring the safety and integrity of the equipment during long-distance transportation.
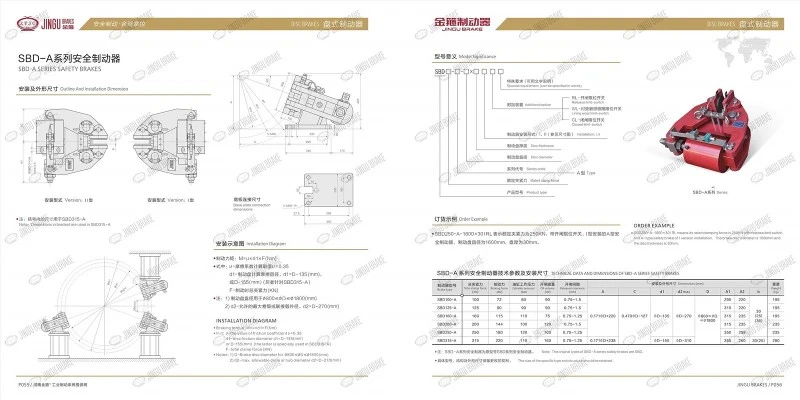
Operating Principle: Fail-Safe and Reliability-First
SBD brakes feature a normally closed, "fail-safe" design, with a core mechanism summarized as "braking upon pressure loss, release upon pressure application":
Braking: In the event of a power outage, loss of pressure, or system failure, the internal high-force disc spring assembly releases its preload, driving the friction pads on both sides to clamp the brake disc. This ensures positive locking, preventing load slippage or drum rotation.
Release: During normal operation, the associated hydraulic power unit supplies oil; the hydraulic pressure overcomes the force of the disc springs, disengaging the friction pads from the brake disc and allowing the equipment to resume operation.

Our company specializes in the R&D, production, and sales of industrial equipment such as drum brakes, safety disc brakes, and hydraulic power units. Our products are widely used in sectors including mining, ports, metallurgy, and construction machinery; they are exported to overseas markets and highly trusted by customers. Please feel free to contact us for further product details or to discuss potential cooperation.